At Mechanical Advantage, two Harperizer centrifugal finishing machines ran daily to deburr metal medical components. The OEM setup relied on slow-threaded fasteners, requiring 1 to 2 minutes per lid during changeovers. Working alongside three other interns, I co-designed and manufactured 10 quick-release replacement lids.
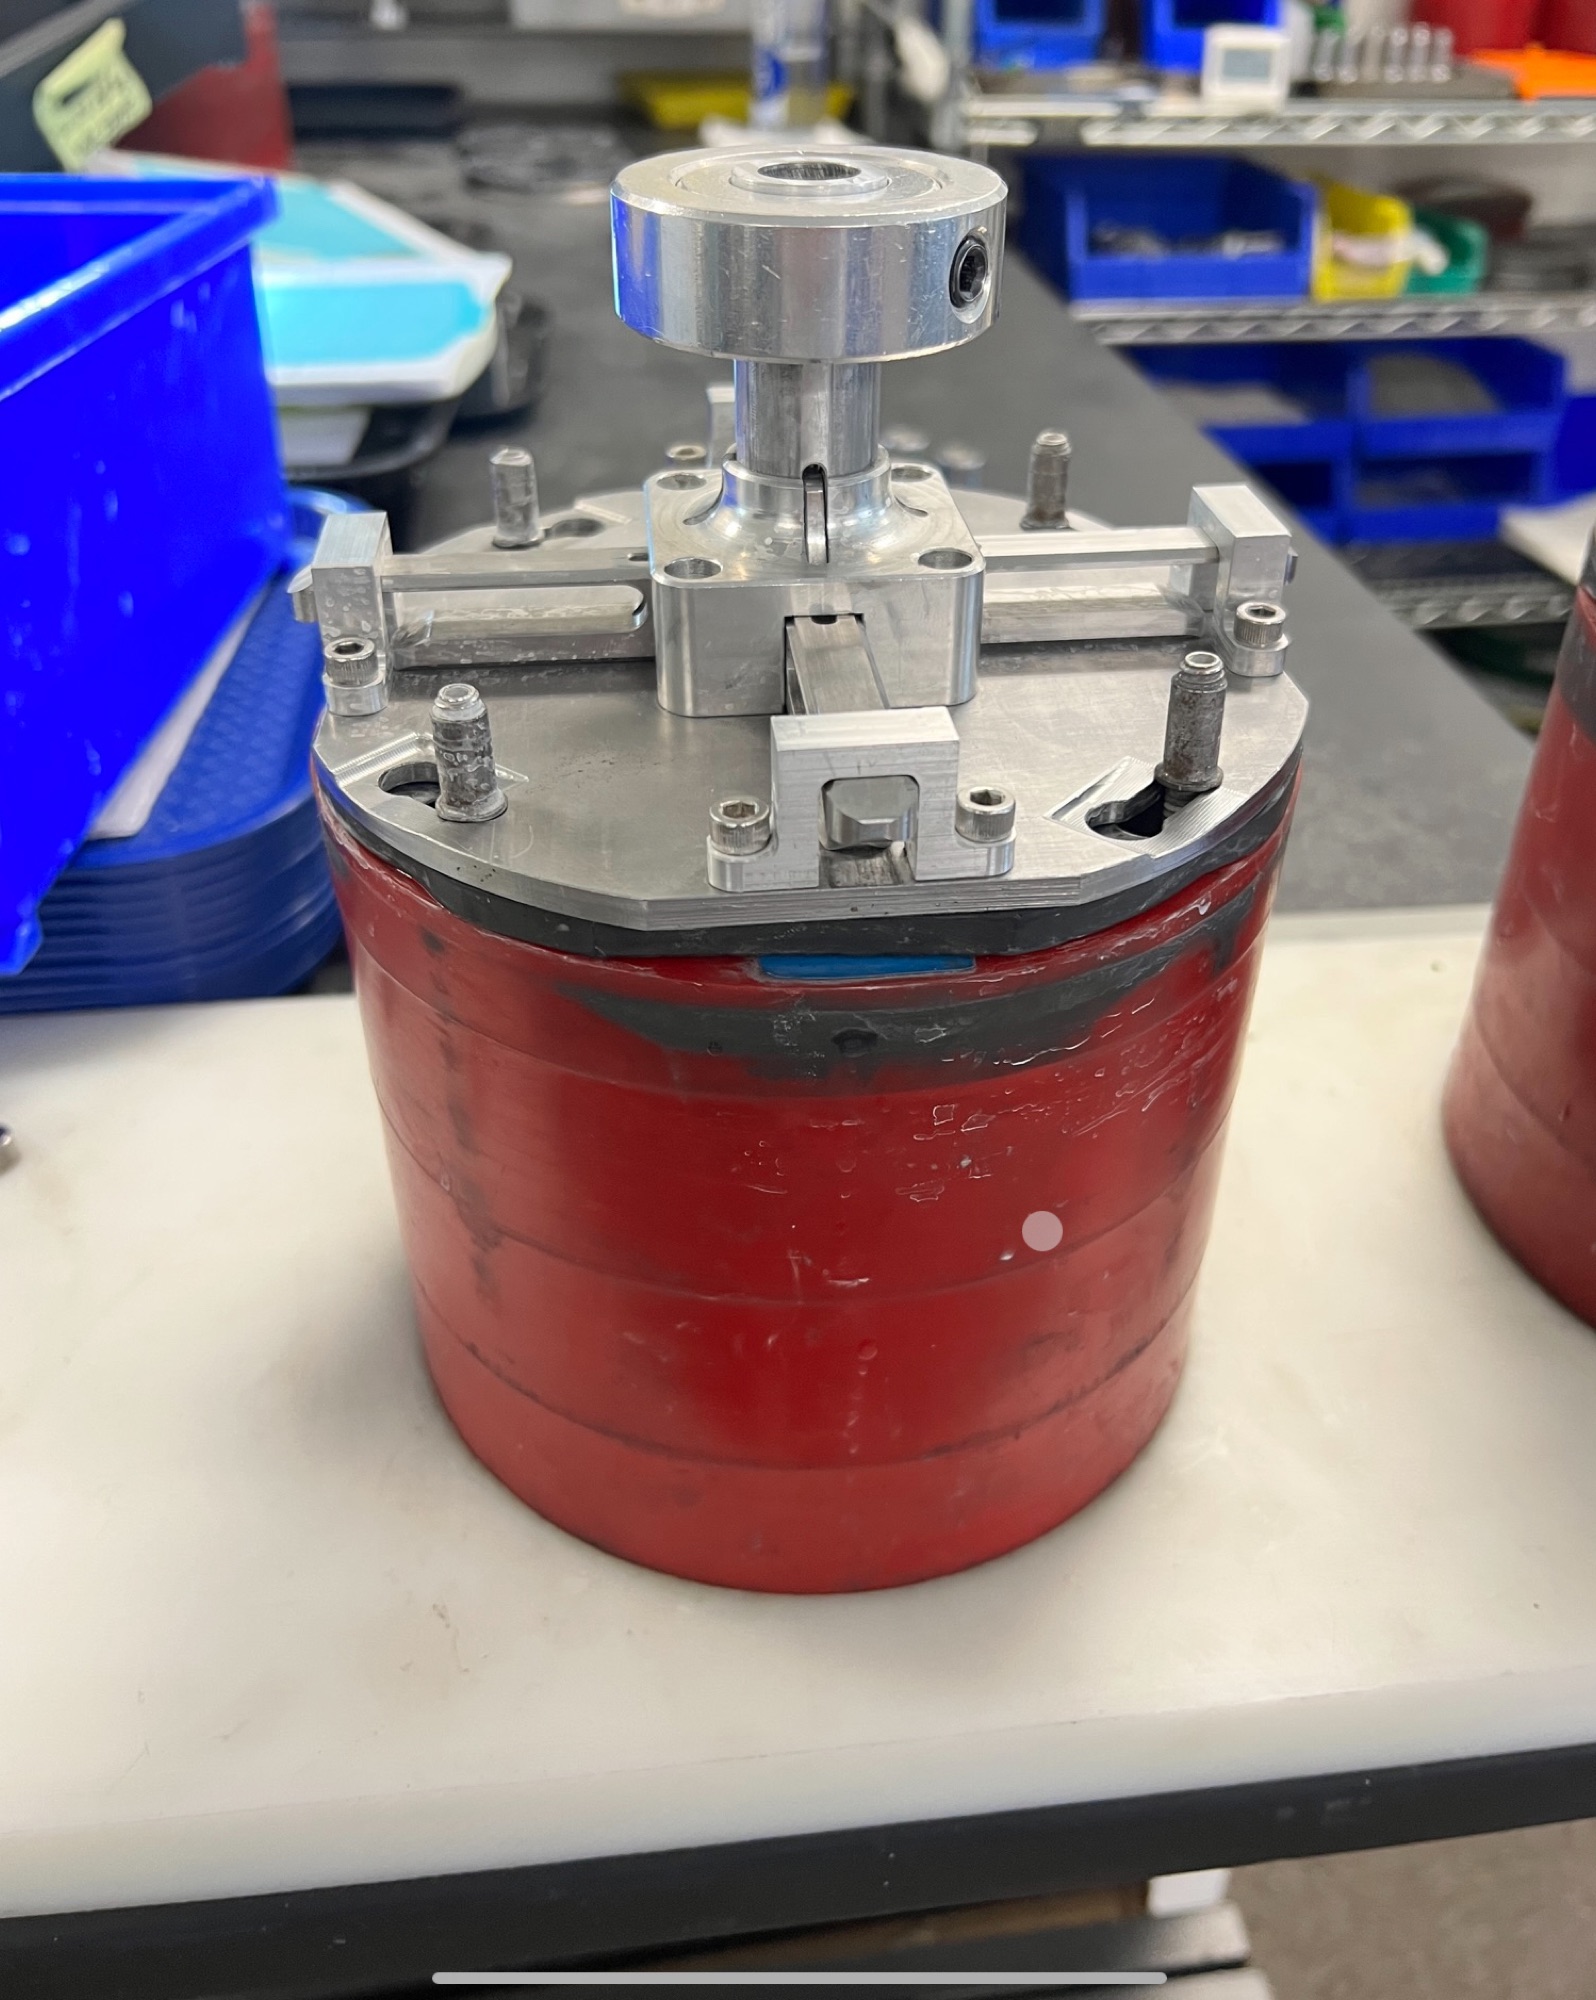
Each lid assembly required 14 custom-machined components, totaling 140 parts across the production run.
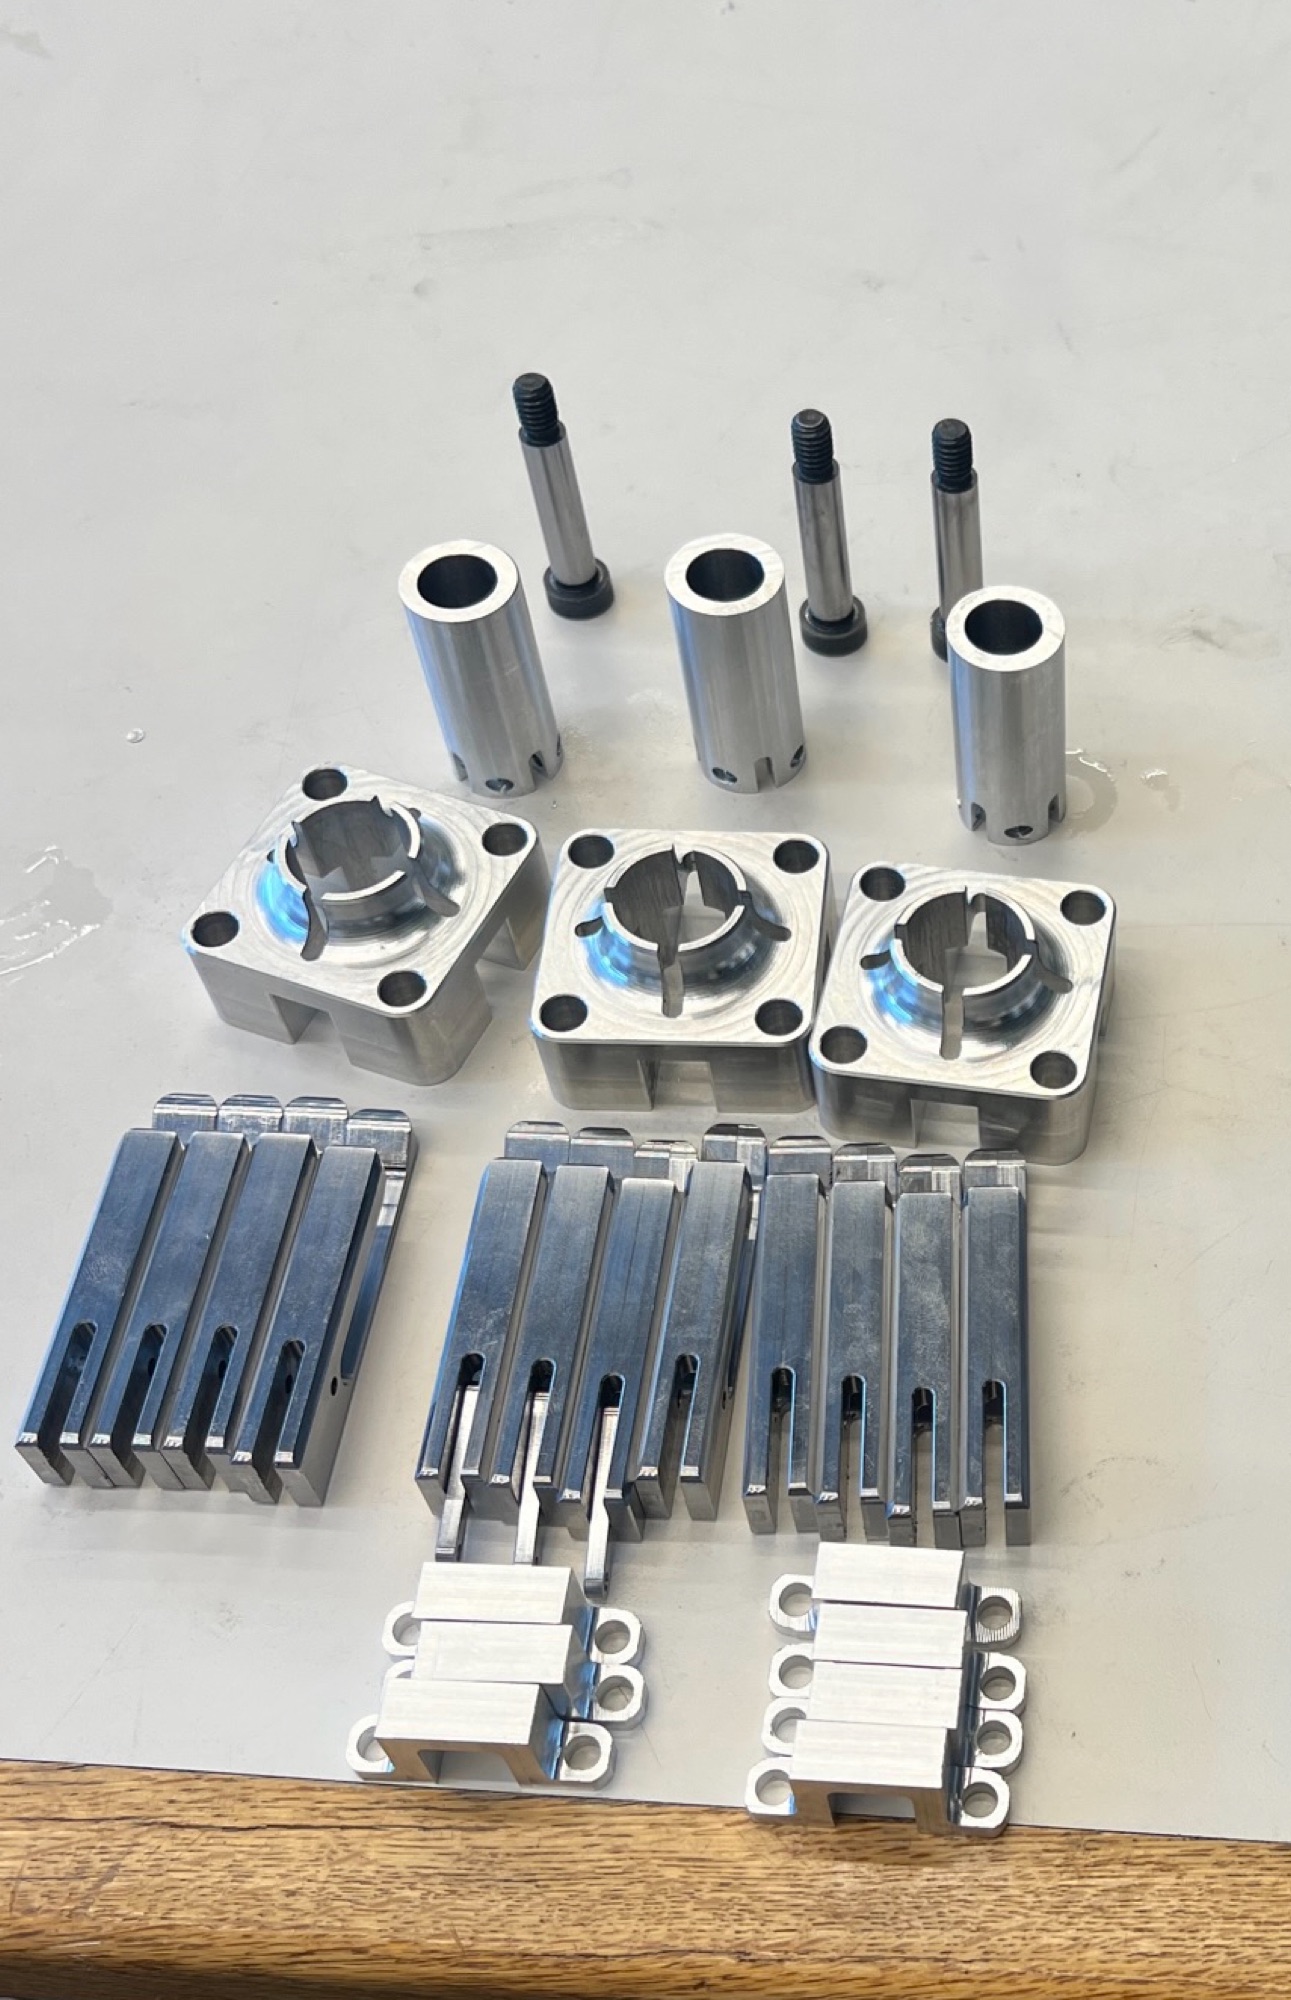
Eliminating The Machining Bottleneck
The primary structural locking element consisted of four 1018 steel clamping claws per lid. Due to the material's machining characteristics, each claw required nearly 2 hours of mill time. With 40 claws total, machining time exceeded 80 hours.
Automated Stock Feeding
To eliminate operator downtime, I designed an automated bar-puller assembly for the 4th axis. The mechanism pulled fresh 1018 bar stock through the spindle between program cycles, enabling lights-out machining overnight and producing complete sets of 4 claws in 8-hour automated runs.